About Us

Trusted Heat Exchanger Manufacturer in India

Company Overview

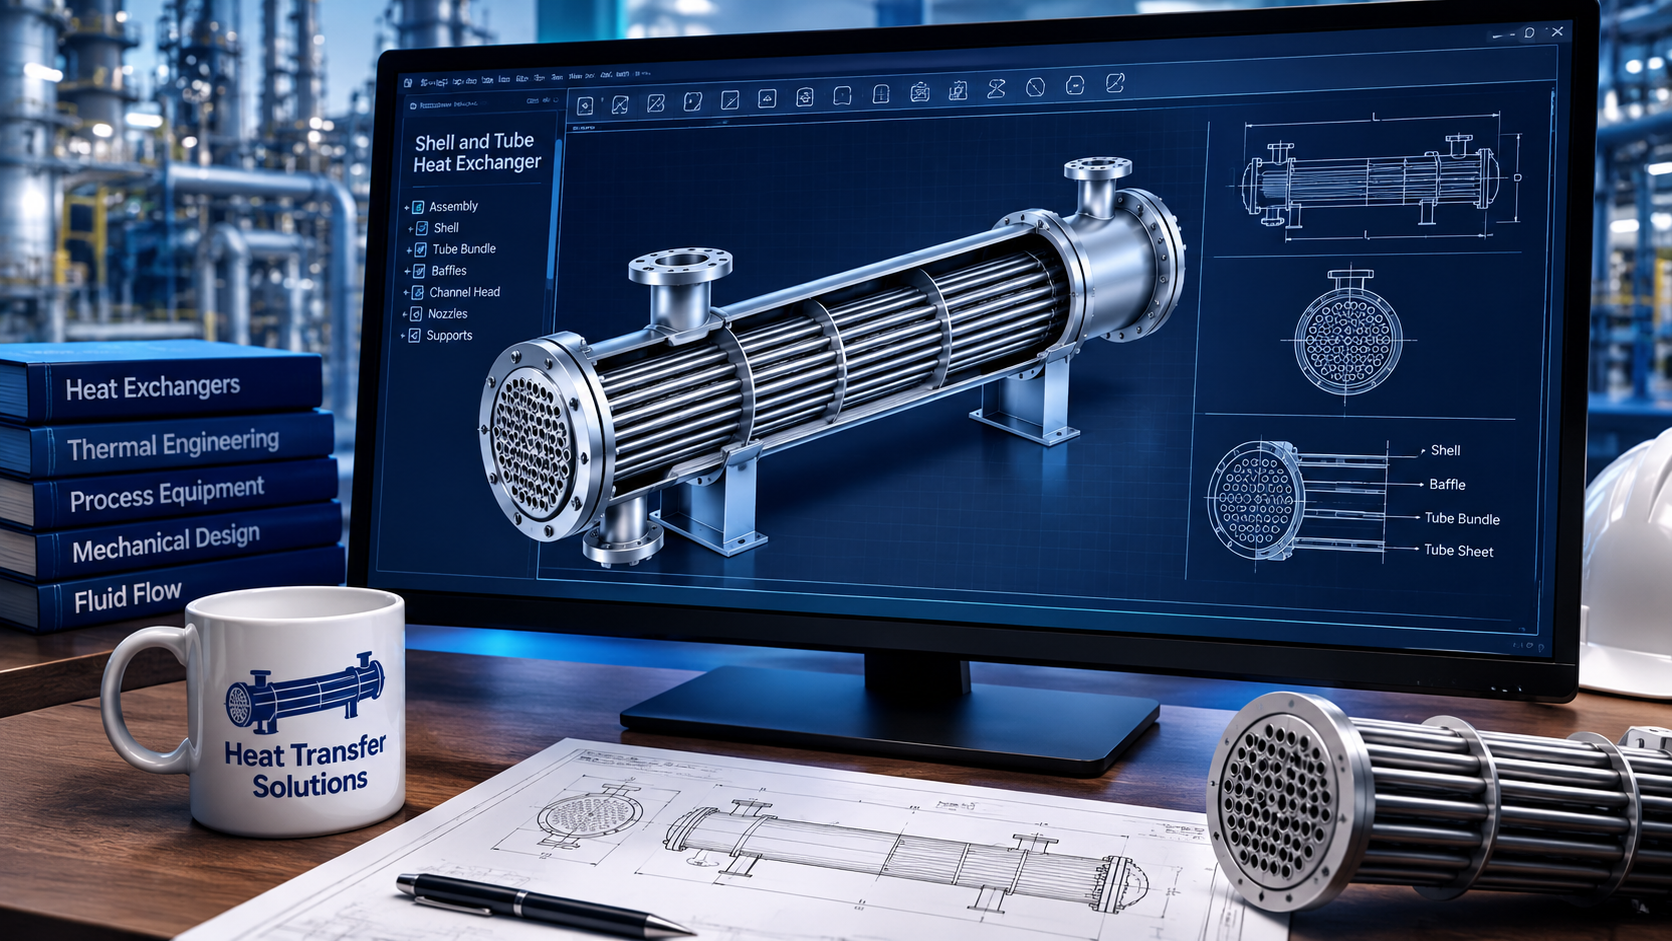
SHE Heat Exchanger is a leading manufacturer and supplier of industrial heat exchangers, committed to delivering high-quality heat transfer solutions for a wide range of industries. With a strong focus on engineering excellence, product quality, and customer satisfaction, we specialize in the design, manufacturing, and supply of Shell & Tube Heat Exchangers, Plate Heat Exchangers, Air Cooled Heat Exchangers, and Oil Coolers.

Our goal is to provide reliable, energy-efficient, and cost-effective solutions that help industries optimize their thermal processes and improve operational performance. Through continuous innovation and advanced manufacturing practices, we strive to meet the evolving requirements of modern industries across India and international markets.

Who We Are

At SHE Heat Exchanger, we believe that every industrial process requires a dependable heat transfer solution. Our team of experienced engineers, designers, and technicians works closely with customers to understand their specific process requirements and deliver customized solutions that ensure maximum efficiency and reliability.

From concept and design to manufacturing, testing, and after-sales support, we maintain the highest standards of quality and professionalism at every stage. Our expertise in heat exchanger technology allows us to provide solutions that perform effectively even in demanding industrial environments.

Over the years, we have built a reputation for delivering products that combine superior performance, durability, and value. Our commitment to excellence has enabled us to establish long-term relationships with customers from various industrial sectors.
Our Vision

To become one of the most trusted and preferred heat exchanger manufacturers by providing innovative, efficient, and sustainable heat transfer solutions that contribute to industrial growth and operational excellence.

Our Mission

Our mission is to design and manufacture high-performance heat exchangers that meet the highest standards of quality, safety, and reliability while delivering exceptional value to our customers.

We aim to:

  • Deliver innovative and energy-efficient solutions.
  • Maintain superior product quality.
  • Build long-term customer relationships.
  • Continuously improve manufacturing processes.
  • Support industries with reliable thermal engineering solutions.
  • Promote sustainable and efficient industrial operations.

Our Expertise

We specialize in manufacturing a wide range of heat transfer equipment designed to meet diverse industrial requirements.

Shell & Tube Heat Exchangers

Engineered for high-pressure and high-temperature applications, our Shell & Tube Heat Exchangers provide reliable and efficient heat transfer performance for demanding industrial processes.

Plate Heat Exchangers

Designed for compactness and efficiency, our Plate Heat Exchangers offer superior thermal performance and energy savings across various industries.

Air Cooled Heat Exchangers

Our Air Cooled Heat Exchangers provide effective cooling solutions without requiring water, making them ideal for locations with limited water resources.

Oil Cooler Heat Exchangers

We manufacture durable Oil Coolers that help maintain optimal operating temperatures in hydraulic and lubrication systems, improving equipment reliability and performance.

Advanced Manufacturing Facility

Our manufacturing facility is equipped with modern machinery, precision fabrication equipment, and advanced production technologies that enable us to produce high-quality heat exchangers efficiently and consistently.

Every stage of the manufacturing process is carefully monitored to ensure compliance with industry standards and customer specifications. Our facility is designed to handle projects of varying sizes while maintaining the highest levels of accuracy and quality.

Manufacturing Capabilities

  • Precision Fabrication
  • Industrial Welding
  • Custom Equipment Mfg
  • Quality Inspection
  • Pressure/Leak Testing
  • Specialized Assembly
Advanced Manufacturing

Quality Assurance

Quality is the foundation of our business. We are committed to delivering products that meet or exceed customer expectations for performance, reliability, and durability. Every heat exchanger undergoes rigorous inspection and testing before delivery to ensure that it performs efficiently under actual operating conditions.

Our Quality Control Process

  • Raw Material Inspection
  • Dimensional Verification
  • Welding Inspection
  • Hydro Testing
  • Pressure Testing
  • Leak Testing
  • Final Performance Inspection

Engineering Excellence

Our engineering team plays a crucial role in developing innovative and customized heat transfer solutions. By combining technical expertise with practical industry knowledge, we design products that maximize efficiency while minimizing operating costs. We utilize advanced engineering principles and thermal design methodologies to ensure optimal performance for each application.

Our Engineering Services Include:

  • Thermal Design Calculations
  • Equipment Selection
  • Process Optimization
  • Material Selection
  • Performance Analysis
  • Technical Consultation
  • Custom Design Development

Industries We Serve

Our products are widely used across multiple industrial sectors where efficient heat transfer is essential for productivity and process control.

Power Generation

Oil & Gas

Chemical Processing

Petrochemical Plants

Pharmaceutical Industry

Food & Beverage Processing

HVAC Systems

Steel Industry

Cement Industry

Marine Applications

Paper & Pulp Industry

Fertilizer Plants

Our extensive industry experience enables us to understand sector-specific requirements and deliver solutions that meet the highest operational standards.

Why Choose SHE Heat Exchanger?

Customized Solutions

We understand that every application is unique. Our team develops tailored solutions based on specific customer requirements.

Experienced Team

Our engineers and technicians possess extensive experience in heat transfer technology and industrial applications.

Superior Product Quality

We use high-quality materials and proven manufacturing practices to ensure reliable performance and long service life.

Competitive Pricing

Our efficient manufacturing processes allow us to provide high-quality products at competitive prices.

Timely Delivery

We value project schedules and work diligently to deliver products on time.

Customer Support

Our commitment extends beyond product delivery. We provide ongoing technical support and assistance whenever needed.

Our Commitment

Our Commitment to Sustainability

Efficient heat transfer systems play a significant role in reducing energy consumption and improving industrial sustainability. At SHE Heat Exchanger, we focus on developing solutions that help industries optimize energy usage while minimizing environmental impact.

Our products are designed to support efficient thermal management, improved process performance, and sustainable industrial operations.

Building Long-Term Partnerships

We believe that success is built on trust, quality, and customer satisfaction. Our objective is not only to supply heat exchangers but also to become a long-term technology partner for our customers.

By understanding customer needs and consistently delivering dependable solutions, we have earned the confidence of clients across diverse industries. We remain committed to continuous improvement, technological advancement, and delivering value through innovative heat transfer solutions.

Partner with SHE Heat Exchanger

Whether you require a standard heat exchanger, a customized thermal solution, or expert technical support, SHE Heat Exchanger is ready to assist.

With a strong commitment to quality, engineering excellence, and customer satisfaction, we continue to deliver reliable heat exchanger solutions that support industrial growth and operational efficiency.

Contact Our Team
Chat with us on WhatsApp