Shell & Tube Heat Exchanger Manufacturer in India
SHE Heat Exchanger is a leading manufacturer and supplier of high-quality Shell & Tube Heat Exchangers designed for efficient heat transfer in demanding industrial applications. Our heat exchangers are engineered to deliver reliable performance, energy efficiency, and long service life while meeting international quality standards.
We manufacture customized Shell & Tube Heat Exchangers for industries such as oil & gas, petrochemicals, chemicals, power generation, pharmaceuticals, food processing, marine, and process industries. Every unit is designed according to customer requirements and applicable standards including ASME, TEMA, and industry-specific specifications.
What is a Shell & Tube Heat Exchanger?
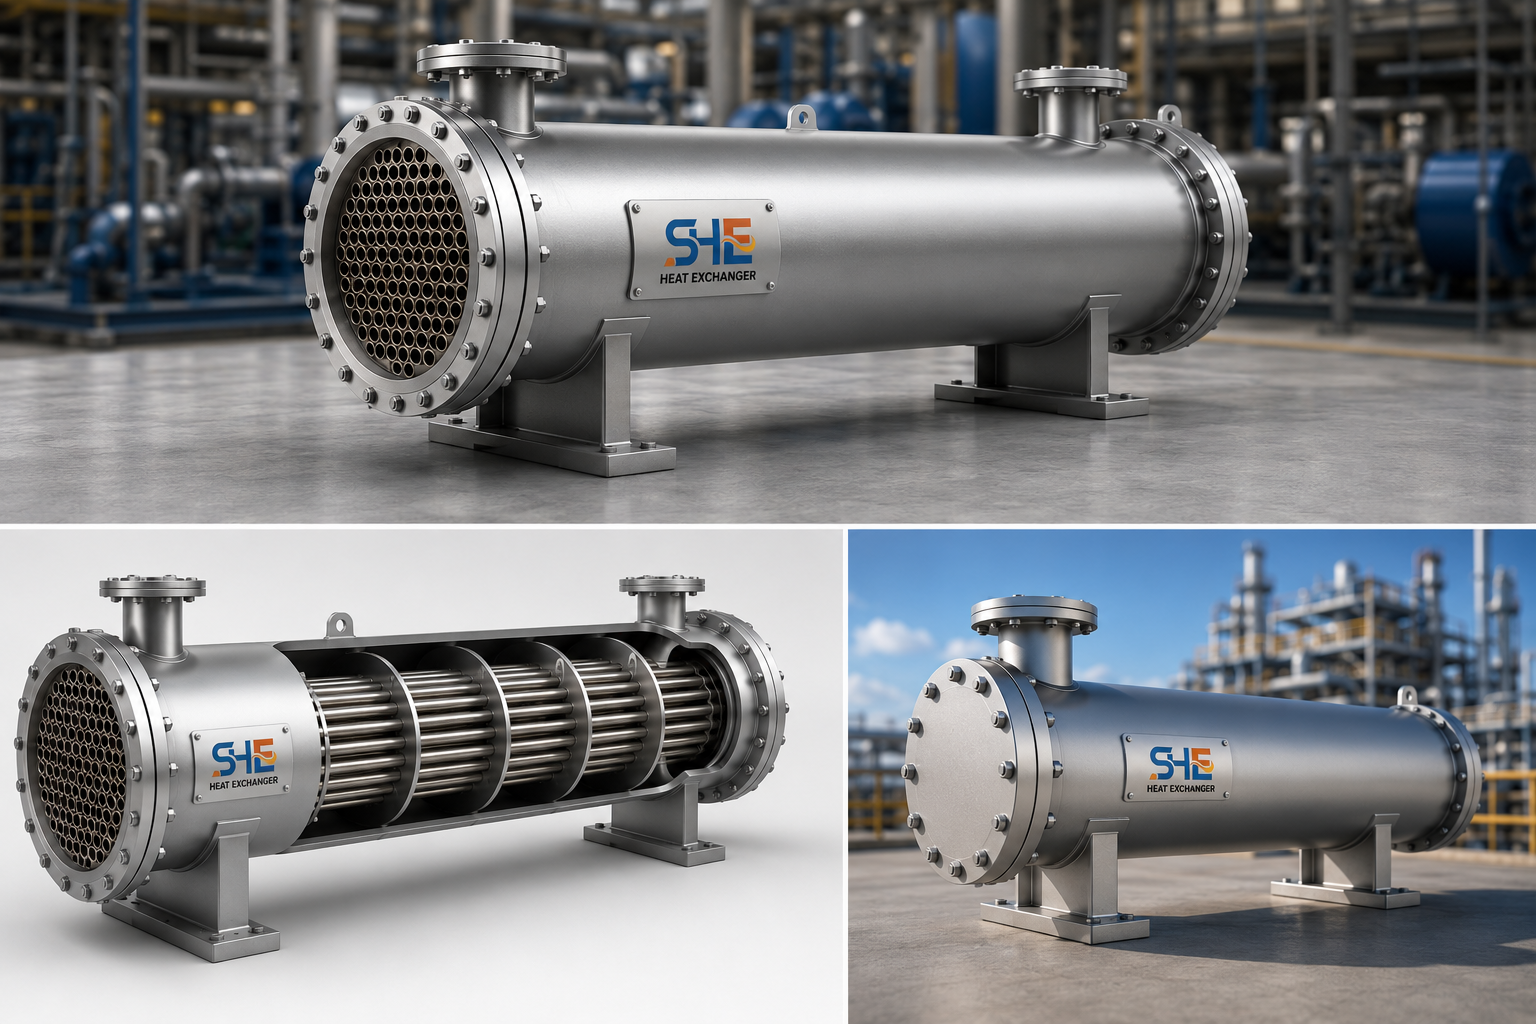
A Shell & Tube Heat Exchanger is a heat transfer device that consists of a bundle of tubes enclosed within a cylindrical shell. One fluid flows through the tubes while another fluid flows through the shell side. Heat is transferred between the two fluids without mixing them.
Due to their robust construction, high pressure handling capability, and excellent thermal performance, Shell & Tube Heat Exchangers are among the most widely used heat transfer equipment across industries.
Key Features
High Efficiency
High Thermal Efficiency
Durable
Rugged and Durable Construction
High Press/Temp
Suitable for High Pressure & Temp Applications
Corrosion Resistant
Corrosion Resistant Material Options
Easy Maintenance
Easy Maintenance and Cleaning
Custom Design
Customized Design as per Process Requirements
Long Life
Long Service Life
Reliable
Reliable Performance in Continuous Operations
Technical Specifications
Types of Shell & Tube Heat Exchangers
Fixed Tube Sheet Heat Exchanger
The tube sheets are permanently welded to the shell. This design is economical and suitable for applications where shell-side cleaning is not frequently required.
U-Tube Heat Exchanger
The tubes are bent into a U-shape, allowing thermal expansion without the need for expansion joints. Ideal for high-temperature applications.
Floating Head Heat Exchanger
Designed to accommodate thermal expansion and facilitate mechanical cleaning of both shell and tube sides. Widely used in process industries.
Kettle Type Heat Exchanger
Primarily used as a reboiler in refinery and chemical processing applications. Suitable for vaporization and boiling duties.
Applications of Shell & Tube Heat Exchangers
Our Shell & Tube Heat Exchangers are widely used in:
Manufacturing Process
At SHE Heat Exchanger, every Shell & Tube Heat Exchanger is manufactured through a strict quality-controlled process. The manufacturing cycle includes engineering review, raw material inspection, tube sheet machining, shell fabrication, tube bundle assembly, precision welding, non-destructive testing (NDT), hydrostatic testing, surface treatment, painting, and final inspection.
All manufacturing activities are performed according to approved drawings, customer specifications, and applicable industry standards to ensure maximum safety, reliability, and thermal performance.
Why Choose SHE Heat Exchanger?
- Custom Design Solutions: Designed specifically for your process requirements and operating conditions.
- Quality Materials: Only certified raw materials from approved suppliers are used in manufacturing.
- Advanced Facility: Our facility is equipped with modern machining, fabrication, welding, and testing equipment.
- Strict Quality Control: Every heat exchanger undergoes detailed inspection and testing before dispatch.
- Experienced Team: Our engineers ensure optimal thermal performance and mechanical reliability.
- Timely Delivery: Efficient project management helps us deliver products within committed timelines.
- Technical Support: We provide complete technical assistance from design selection to installation support.
Product Gallery
Frequently Asked Questions
What is a Shell & Tube Heat Exchanger used for?
It is used for transferring heat between two fluids in industrial heating, cooling, condensing, and evaporation applications.
Which industries use Shell & Tube Heat Exchangers?
Oil & gas, petrochemical, power generation, chemical, pharmaceutical, food processing, and marine industries commonly use them.
Can you manufacture customized heat exchangers?
Yes, we manufacture customized heat exchangers according to customer specifications and process requirements.
What materials are available?
We offer Carbon Steel, Stainless Steel, Duplex Stainless Steel, Titanium, Copper Nickel, Hastelloy, and other special alloys.
Do your heat exchangers comply with international standards?
Yes, our products can be manufactured according to ASME, TEMA, API, and customer-specific requirements.
Do you provide testing and inspection reports?
Yes, complete quality documentation, inspection reports, and test certificates are provided with every project.